Points clés
- Define the webbing and buckle as one assembly, not two catalog parts.
- Approve measurable construction evidence before approving color.
- Test the failure mode created by the intended end use; one strength result cannot stand in for edge, color or buckle performance.
Start with a construction stack, not a fabric name
The first buyer decision is the construction stack: fiber route, yarn form, weave, finished width, finished thickness, surface finish and color method. “Nylon webbing” identifies a material family, not a finished belt. Two webbings with the same nominal width can feed through the same buckle differently because thickness, surface friction and compressibility are different.
Put each layer on the approved specification and attach the supplier evidence used to approve it. The DLA record confirms that MIL-DTL-4088 is an active specification for woven nylon webbing. This article cites that scope only; it does not claim that a fashion belt is military compliant or import the specification’s acceptance values into a commercial belt program.
Choose a fiber route from the product brief
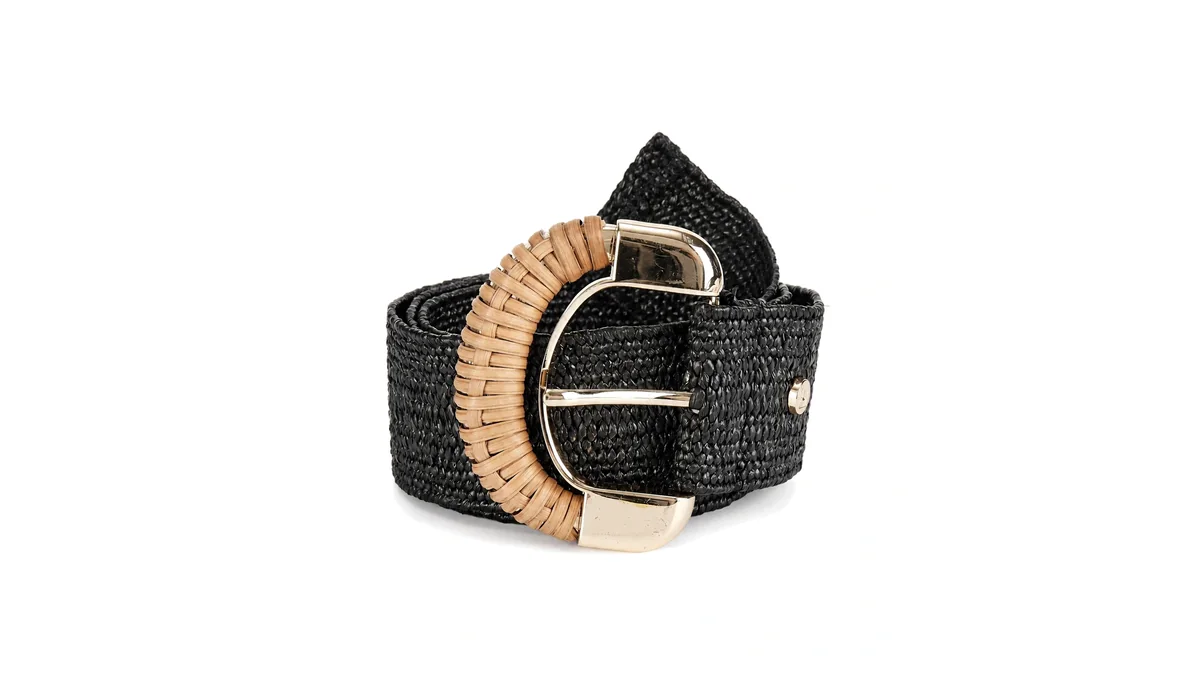
Nylon, polyester, polypropylene and cotton-rich constructions can all appear in belt programs. The commercial choice should begin with the desired hand, appearance, care route, abrasion exposure, color target and buckle mechanism. The correct question is not “which fiber is best?” but “which construction remains stable in this assembly and use case?”
Ask for the exact fiber declaration and the finishing route. If a softener, coating or wash changes surface friction, it can change buckle holding behavior. A recycled-content request also needs chain-of-custody evidence and an approved declaration; visual resemblance is not proof of content.
A current narrow-fabric manufacturer’s data distinguishes polyester as a low-elongation route, polyamide/nylon as a high-elongation route, polypropylene as water-resistant with low elongation, and cotton as highly absorbent. Those are supplier-level material tendencies, not finished-belt guarantees. The weave, yarn grade, finish and assembly can change the result, so the buyer still approves the production-intent construction.
| Candidate route | Verified supplier-described tendency | Belt decision | Evidence to approve |
|---|---|---|---|
| Polyamide / nylon | High elongation; abrasion-resistant | Check whether stretch and recovery support or undermine buckle holding | Fiber declaration, finished swatch, elongation and assembly test |
| Polyester | Low elongation; abrasion- and water-resistant | Candidate where dimensional stability and care route matter | Fiber declaration, color/care evidence and assembly test |
| Polypropylene | Water-resistant; low elongation | Check hand, thickness, positioning and end treatment | Finished construction and cut-end sample |
| Cotton | High absorbency; natural fiber | Check care, dimensional change, cut end and wet handling | Fiber/blend declaration, care test and finished end sample |
Read the weave as a load path
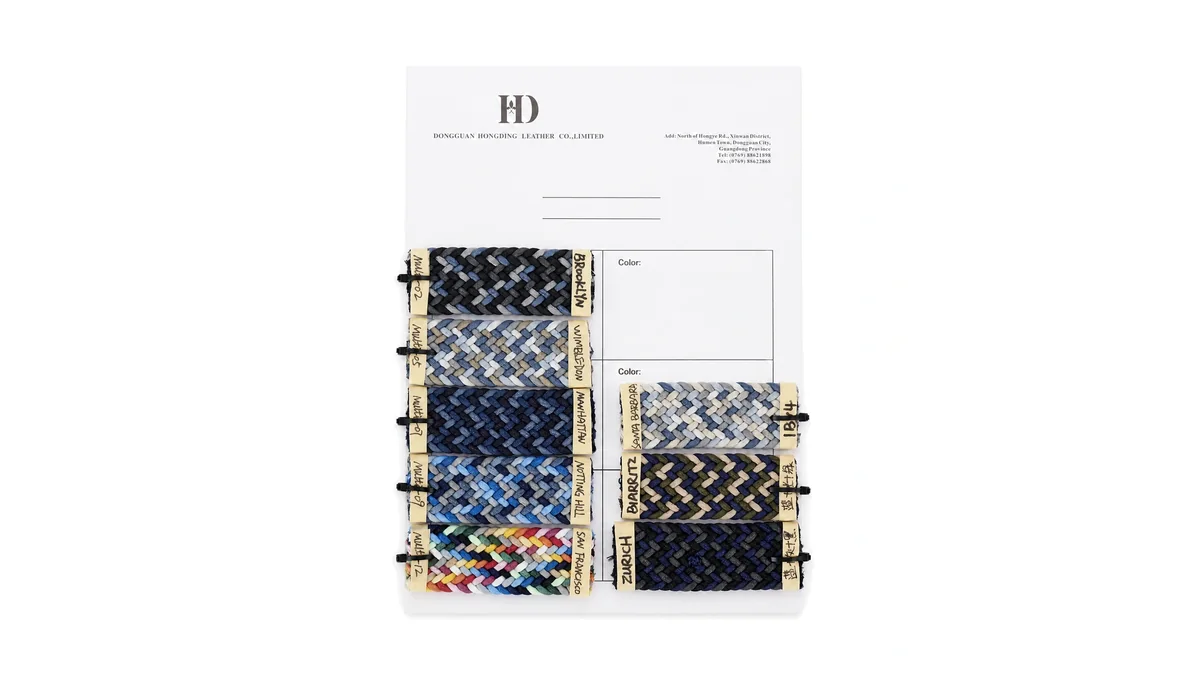
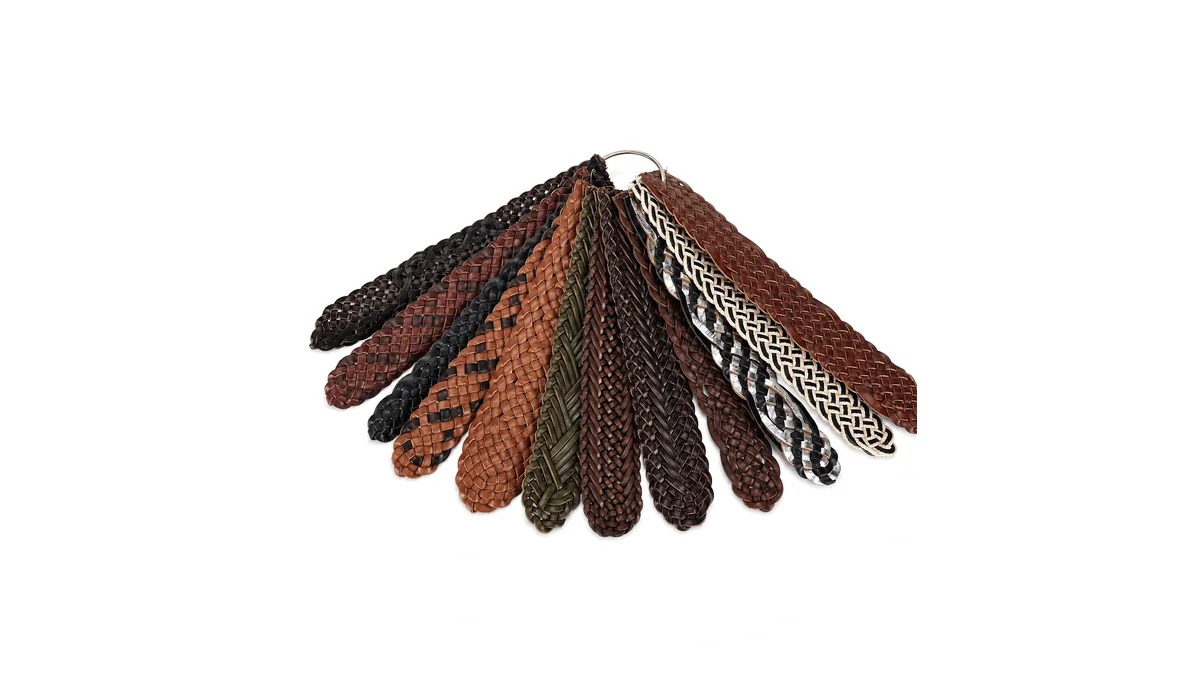
A buyer can examine picks, warp alignment, face pattern, edge formation and local density changes without pretending that a visual count is a universal performance grade. Dense-looking fabric may still elongate, and a decorative face may hide a different load-bearing structure. Use the weave drawing or retained sample to define what may not change.
Supplier construction references list plain, pebble, twill, herringbone, satin and tubular routes. They are not performance grades. Plain/twill/herringbone describe interlacing or visible pattern; tubular describes an overall closed architecture. John Howard’s construction glossary also distinguishes warp yarns running lengthwise, each crosswise insertion as a pick, selvage as the non-raveling edge, and needle-loom versus shuttle-loom edge formation. Freeze the supplier’s actual construction reference instead of approving a style name alone.
Record yarn fiber and form, warp-end arrangement, pick record, layer or tube architecture, loom/edge construction, face direction, repeat, finished width, thickness and the retained physical reference. Then record what happens at the intended bend, clamp, seam or perforation. This turns “dense woven strap” into a change-controlled specification: if the supplier alters yarn, picks, edge or finish, the affected elongation, bend appearance and buckle checks reopen.
Engineer width, thickness and buckle clearance together
Nominal buckle width is not enough. The factory must check the webbing’s actual finished width and compressed thickness against the frame, bar, clamp teeth, roller or friction path. Too much lateral clearance encourages skew; too little creates rubbing. Too much thickness can prevent closure; too little can reduce holding force.
Use a calibrated width instrument and the agreed thickness contact condition; record the instrument and method. Measure minimum, nominal and maximum webbing samples across the production-intent roll positions defined by the program, then measure the smallest hardware opening from the approved hardware lot. Assemble the widest/thickest credible webbing with the tightest hardware, operate the mechanism, apply the program-set load and duration, and record feed force, skew, edge rub, slip and failure mode. Repeat with the narrowest/thinnest condition to expose loss of holding force. The buyer—not this article—sets sample count and acceptance values.
No universal clearance is inserted because buckle mechanisms differ. The drawing should carry the project-specific limits derived from physical samples. If finish, thickness, webbing source or hardware tooling changes, repeat the affected measurement and assembly load checks before approval.
| Stack field | Record at approval | Check |
|---|---|---|
| Webbing width | Minimum / nominal / maximum measured | Feed, lateral skew, edge rub |
| Compressed thickness | Measured under the agreed contact condition | Closure and friction path |
| Hardware opening | Minimum measured opening | Tightest feed condition |
| Free clearance | Hardware opening minus compressed webbing thickness | Project-specific; no universal target |
| Holding result | Load, duration, slip and failure mode | Finished assembly, not loose components |
Separate woven-edge quality from cut-end finishing
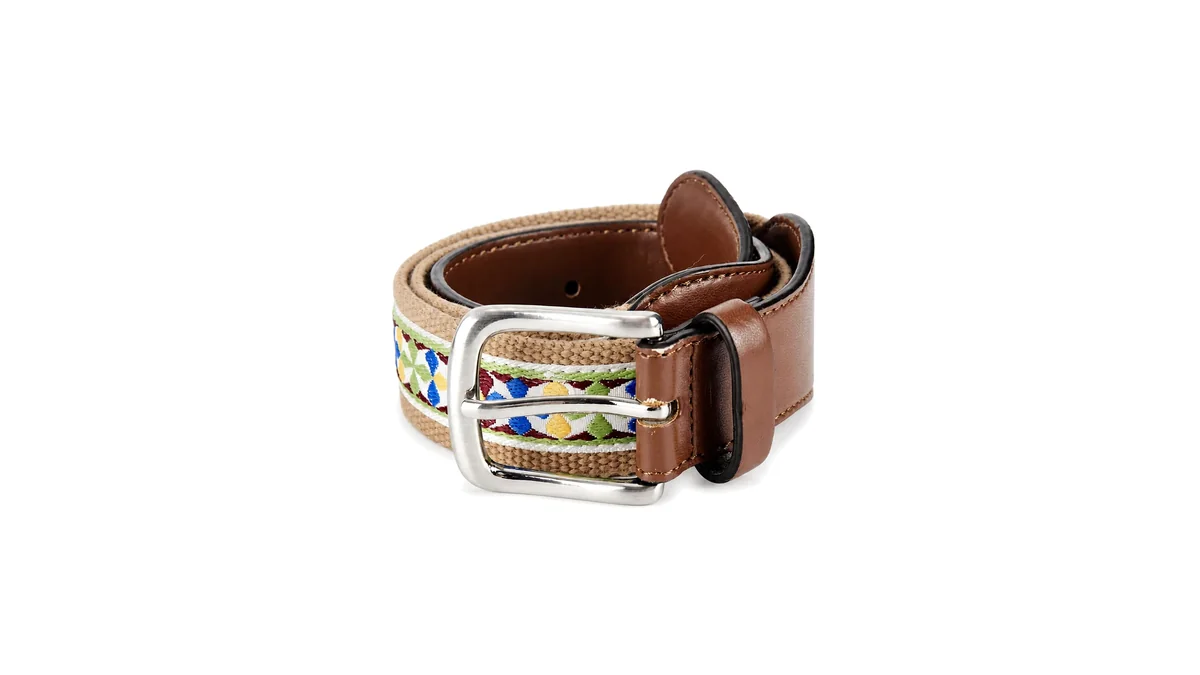
A woven selvage, heat-cut edge and folded or capped termination solve different problems. A selvage controls the long edge. The cut end still needs a treatment compatible with the fiber and appearance standard. Heat treatment can stabilize thermoplastic yarns, but excessive heat can leave a hard, glossy or distorted edge. Cotton-rich constructions need a different solution.
Inspect edge waviness, loose filaments, sharpness, discoloration and thickness at the buckle path. Then test the actual end construction—folded, stitched, clamped, capped or combined—because the termination introduces failure modes that an untouched roll sample cannot reveal.
Use a test matrix instead of one “strength” result
ISO 13934-1 provides a strip method for maximum force and elongation of textile fabrics. ISO 105-X12 addresses color fastness to rubbing, and ISO 105-C06 addresses domestic and commercial laundering. These methods answer different questions. A tensile result cannot predict crocking; a rubbing result cannot prove buckle retention.
Map each risk to a method, specimen condition and acceptance criterion set by the program. Include the finished assembly where the buckle or stitched tab changes the load path. When no published method fits the exact mechanism, document an internal comparative test with fixture, cycle, conditioning and failure definition rather than reporting an unexplained pass.
| Failure risk | Method / scope | Specimen and condition | Acceptance field | Responsable |
|---|---|---|---|---|
| Break or excessive elongation | ISO 13934-1 where applicable | Declared strip specimen and conditioning | Program-set value | Quality |
| Dry/wet rubbing transfer | ISO 105-X12 | Approved color and stated rubbing condition | Program-set grade | Material owner |
| Laundering change | ISO 105-C06 when care route requires it | Finished color/construction and stated cycle | Program-set grade/change | Product team |
| Buckle slip or feed | Documented internal assembly method | Production-intent webbing and buckle | Maximum slip/failure definition left blank | Engineering / quality |
| End fray or hard edge | Documented handling or flex comparison | Finished cut end and termination | Visual/functional acceptance reference | Product team |
Approve in three evidence gates
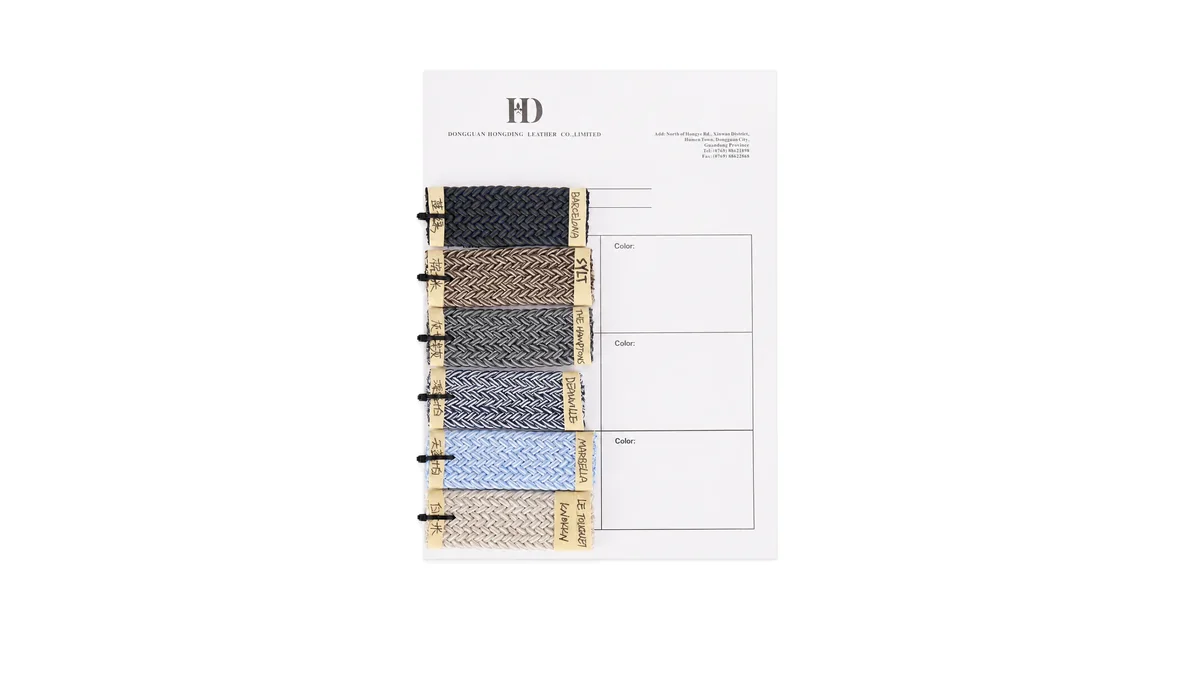
Gate one is the component swatch: construction, color, face direction and basic test evidence. Gate two is the assembled belt: feeding, locking, folding, sewing and end finish. Gate three is the pre-production sample made with production-intent materials and hardware. Each gate should close named questions before the next spend is released.
HongDing’s documented process includes material and hardware sourcing, physical sampling, manufacturing and QC. The Product Bible gives a typical physical-sample window of two to three weeks once inputs are clear; treat that as a planning reference, not a promise detached from material availability or approvals.
Send an RFQ that prevents silent substitutions
- Fiber declaration and any verified content claim
- Weave reference, approved face and color standard
- Finished width, thickness and roll-to-roll tolerance
- Buckle drawing plus actual mating sample
- Long-edge and cut-end treatment
- Assembly method and seam or clamp requirements
- Required test methods, specimen condition and acceptance rules
- Packaging, labeling and review responsibilities
Do not ask for a price against an undefined “similar webbing.” The RFQ should identify which properties are frozen and which may be optimized. Link the approved bill of materials to the color sample and assembly sample so a later yarn, finish or buckle change triggers revalidation.
What a buyer should approve before bulk
Approve the assembly that manages the intended risk: stable geometry, believable hardware mechanics, clean edges, controlled color and documented evidence. Keep one signed reference sample and one production control sample. If the program changes the webbing finish or buckle source, reopen the affected interface checks.
For a factory review that joins textile selection, buckle sourcing and assembly controls, use HongDing’s belt manufacturing capabilities as the commercial route. Related guides cover braided versus woven belts, buckle mechanisms et pre-production samples.
Verified source notes
- MIL-DTL-4088 webbing specification
- ISO 13934-1 tensile method
- ISO 105-X12 rubbing fastness
- ISO 105-C06 laundering fastness
- Webbing Products custom webbing data
- John Howard webbing-construction glossary
Questions fréquentes
What should a webbing belt specification include?
State the fiber declaration, weave reference, finished width and thickness, color standard, edge and cut-end treatment, buckle drawing, assembly method, test methods and approval samples.
Is dense webbing always stronger?
No. Visual density alone does not establish maximum force, elongation, abrasion behavior or buckle retention. Use an appropriate test and the finished assembly.
Can one buckle fit every webbing of the same width?
No. Finished thickness, compressibility, surface friction and the buckle path can change feeding and holding behavior even when nominal width matches.
Which ISO tests are useful?
ISO 13934-1 addresses maximum force and elongation by a strip method; ISO 105-X12 covers rubbing fastness; ISO 105-C06 covers laundering fastness. Select only methods relevant to the product brief.