Points clés à retenir
- Personne ne fabrique les deux pièces. Les sangles viennent du monde du cuir et du textile ; les boucles viennent de la fonte, de l’emboutissage et du placage des métaux. Chaque ceinture vendue en gros est un produit assemblé — la vraie question est de savoir qui maîtrise l’interface.
- La quincaillerie est validée sur la sangle, jamais sur un bureau. Une boucle qui passe l’inspection seule peut encore faire échouer la ceinture : ajustement ardillon-trou, jeu du cadre par rapport à l’épaisseur de la sangle, pose des rivets, équilibre du poids. Validez la quincaillerie comme un système, pas comme une pièce.
- Un approvisionnement séparé cumule les MOQ et répartit les responsabilités. Le minimum d’un fournisseur de quincaillerie plus le minimum d’une usine de sangles plus un lot d’assemblage — et lorsque la combinaison échoue, chaque fournisseur pointe la pièce de l’autre.
- La quincaillerie sur mesure suit un parcours fixe. Modèle 3D/CAO, puis moule, puis échantillons de première pièce testés sur la sangle de production. Le coût et les délais de l’outillage sont propres au projet et doivent figurer dans un devis écrit avant toute découpe de métal.
- Le placage est une spécification, pas une humeur. Le type de placage, la référence de couleur approuvée, les limites de rayures, le contrôle de corrosion et l’approbation du lot sont consignés par écrit avant la production — les finitions de la quincaillerie sont le point où les programmes de ceintures non testés échouent en masse.
Ce que couvre ce guide
- En quoi se décompose réellement le commerce de gros des ceintures et des boucles
- La règle du système : une boucle est validée sur la sangle
- Approvisionnement séparé vs approvisionnement du système
- Le risque de mélange : là où les combinaisons non testées échouent
- Un cas pratique : le programme mixte qui s'est disloqué
- Quincaillerie sur mesure : le parcours modèle 3D → moule → échantillon
- Spécifications de placage et de surface
- Logique de MOQ lorsque vous achetez les pièces séparément
- Assembler en interne ou acheter des ceintures finies ?
Une ceinture finie, ce sont deux chaînes d'approvisionnement dans un seul polybag. La sangle a commencé comme une peau ou un rouleau de textile dans une tannerie ou une usine de tissage ; la boucle a commencé comme une pièce de fonderie ou d'estampage dans une fonderie de quincaillerie, puis est passée par le polissage et le placage. Lorsque les acheteurs recherchent des ceintures et des boucles en gros, la plupart ne cherchent pas deux fournisseurs — ils se posent une question de décision : dois-je acheter les pièces ensemble comme un seul produit, ou séparément comme composants et prendre en charge moi-même l'assemblage ?
En bref : la quincaillerie ne peut pas être approuvée indépendamment du système de ceinture. Les sangles et les boucles viennent d'industries différentes, et la ceinture ne fonctionne qu'à l'interface entre elles — de l'ardillon au trou, du cadre à l'épaisseur de la sangle, du rivet au matériau. Les sourcer comme un seul système, auprès d'une usine qui développe et teste la combinaison, est la norme pour les programmes de vente au détail ; les sourcer séparément ne vaut la peine que lorsque vous maîtrisez déjà les conceptions de quincaillerie et disposez d'une capacité d'assemblage.
Ce guide couvre les deux voies, les risques de mélange entre les deux, le parcours de quincaillerie sur mesure du modèle 3D au moule puis aux échantillons, ainsi que les mécanismes de placage et de MOQ que la plupart des acheteurs apprennent à leurs dépens.
HongDing assure le développement et la fabrication de ceintures sur mesure pour les marques, détaillants, grossistes et équipes d'approvisionnement, et le développement de boucles — modélisation 3D/CAO, moules, premiers articles — fait partie de ce périmètre de développement. Cela nous place du côté intégré de ce débat, et nous vous dirons quand même où la voie séparée est le bon choix.
En quoi se divise réellement le commerce de gros des ceintures et des boucles
Aucune usine au monde ne coule ses propres boucles et ne découpe ses propres sangles à grande échelle. La quincaillerie métallique appartient à une industrie de fonderie et de placage avec ses propres outillages, minimums et logique de lots ; les sangles appartiennent à l'industrie du cuir et du textile, avec des logiques entièrement différentes. Même un fabricant de ceintures qui développe sa quincaillerie en interne achète le métal à cet univers de la quincaillerie — la différence réside dans qui le spécifie, qui le teste sur la sangle et qui répond lorsque la combinaison échoue.
Sous cette expression de recherche se cachent trois achats différents, et les confondre fait perdre du temps à tout le monde :
- Ceintures finies, quincaillerie incluse — vous achetez un produit assemblé selon un cahier des charges, et un seul fournisseur gère la sangle, la boucle, l'assemblage et l'emballage comme un seul SKU. C'est la voie du programme de vente en gros.
- Sangles ou ébauches plus boucles comme composants — vous achetez des pièces auprès de deux fournisseurs et les assemblez vous-même ou via un tiers : la voie des composants, et un jeu de spécialiste.
- Boucles et quincaillerie uniquement — fabricants de sangles, marques artisanales et circuits de réparation. Un achat tout à fait différent ; ce guide ne le couvre pas.
Ce guide couvre la décision entre les deux premières. Si vous assemblez vos propres ceintures, lisez deux fois la section sur le mélange — elle est écrite pour vous.
La règle du système : une boucle est approuvée sur la sangle, jamais sur un bureau
Les plombiers l’ont appris il y a des décennies : un tuyau et un raccord sont, chacun, des pièces fabriquées et certifiées, et un joint entre eux peut encore fuir. Ce qui échoue n’est aucune des deux pièces — c’est l’interface que personne n’a testée. Une boucle et une sangle relèvent de la même classe de problème. Le monde de la quincaillerie peut livrer une boucle plaquée qui respecte tous les plans dimensionnels, l’usine de sangles une sangle coupée et cousue — et la ceinture qu’elles forment ensemble peut encore se défaire dans les mains d’un client.
L’interface est une spécification physique, et elle a de vraies dimensions :
- Ardillon par rapport au trou — diamètre de l’ardillon par rapport à la taille du trou poinçonné, et espacement des trous par rapport à la géométrie de la boucle.
- Dégagement du cadre — dégagement interne par rapport à l’épaisseur de la sangle, y compris la peinture des bords ou le pli, pas seulement la jauge nominale.
- Engagement du bouton-pression, de l’anneau et du passant — la résistance du bouton-pression et l’ajustement du passant supposent une sangle dans une plage d’épaisseur.
- Pose de rivets et de vis — force de réglage adaptée au matériau de la sangle ; une force réglée pour du cuir de 3,0 mm se desserre sur du 3,8 mm ou le déchire.
- Poids et équilibre — une boucle à plaque lourde sur une sangle fine traîne, oscille et déchire les trous avec le temps.
Aucun de ces problèmes n'apparaît lorsque la boucle est inspectée seule sur la table d'un vendeur. C'est la règle fondamentale du guide : la quincaillerie ne peut pas être approuvée séparément du système de ceinture avec lequel elle est expédiée. If a supplier offers to send you approved buckles and approved straps that have never been assembled together, what you are buying is two approved parts and one unapproved product.
Separate Sourcing vs. Sourcing the System
Both routes are legitimate; they suit different buyers. The table is the short version — the trade-offs behind each row run through the rest of this guide, so read both before choosing.
| Dimension | Buckles from a hardware vendor + straps from a factory | Straps and hardware sourced as one system |
|---|---|---|
| Who owns the interface | You do — you spec hole size, thickness tolerance, snap and rivet positions, and you arbitrate when the two suppliers disagree | The factory — the strap is built to the hardware and the combination is tested before approval |
| MOQ behavior | Two or three minimums stack: hardware MOQ per finish, strap MOQ per material, plus an assembly batch | One program MOQ, confirmed after material, construction, SKU mix and packaging are defined |
| Tooling | You may own the buckle mold and manage the hardware vendor’s revisions yourself | Tooling is developed inside the program (3D model → mold → samples), cost and timing quoted per project |
| QC boundary | Hardware inspected alone at the vendor, strap inspected alone at the factory; the combination often untested until it reaches you | Hardware inspected on the belt: fit, function, plating and packaging checked as one product |
| When the combination fails | Each supplier can blame the other’s part; root-cause analysis is your project | One supplier owns the failure and the fix |
| Reorder consistency | Two supply chains to keep aligned — plating batch drift on one side, material lot drift on the other | A golden sample per SKU covers the whole assembled belt, hardware included |
| Best fit | Buyers who already control hardware designs, hold assembly capability, or must use a specific hardware design | Custom belt programs, retail launches, seasonal reorders where the belt ships as one SKU |
The honest verdict: without a hardware engineer and assembly capability on your side, separate sourcing is not a cost saving — it is a coordination job you just bought. The component route earns its keep in specific cases, and the custom hardware section below covers the main one.
The Mixing Risk: Where Untested Combinations Fail
The structural problem with the component route is a hole in QC coverage shaped exactly like the interface. The hardware vendor’s inspection covers casting quality, plating and dimensions against the drawing. The strap factory’s inspection covers cutting, stitching, edge work and hole positions against its spec. Neither covers the belt. The combination gets its first real test when a customer fastens it — the most expensive test bench in the industry.
The failure modes that come out of that hole in coverage are consistent:
- Loose hardware after assembly or wear — rivets and snaps set to a force that suits one thickness, applied to another.
- Function failure — a prong that seats between holes, an automatic or ratchet mechanism that will not engage on the specified strap, a roller that binds.
- Plating damage at assembly and in transit — hardware scratched against setting fixtures, or buckles packed bare against straps.
- Fit friction — a frame that pinches a strap after edge paint adds thickness, so the buckle crooks sideways and the plating wears at the contact point.
- Hole elongation and tearing — holes punched for one prong diameter and strap gauge, loaded by another.
Every one of these is a system failure, not a part failure. Each part passed its own inspection; the product still failed. That is the mixing risk in one sentence.
A Worked Scenario: The Mixed Program That Came Apart
A composite of a pattern we see often, with the details changed: a mid-size retailer launches a workwear belt line. They source roller buckles from a hardware vendor they trust — good plating, their own spec, the parts pass incoming inspection. Straps come from a strap factory that cuts, stitches and edge-paints to spec, and the straps pass too. A third party joins the two, punching holes to a standard size chart.
The first shipment generates returns within a season. The edge paint on the straps runs thicker than the buckles’ frame clearance, so the buckles sit crooked and the plating wears through at the contact point. On the smaller sizes, the prong diameter against the punched hole size lets the prong slide between holes under load. Both suppliers are technically right — the buckles meet the drawing, the straps meet the spec — and diagnosing the product takes weeks of samples between two factories that have never spoken.
The fix is structural, not cosmetic. The program moves to system approval: the buckle vendor’s first articles are mounted on production straps — the actual material and edge paint — and one golden sample is approved for the assembled belt. Function limits go in writing: the prong must seat in every hole, the frame must clear the strap freely, no plating contact marks after an agreed flex check.
Reorders then repeat against that golden sample, and the failure mode disappears from the return log. The lesson generalizes: the parts were never the problem; the untested combination was.
Sourcing buckles and straps for the same program?
Bring your buckle reference or logo artwork, the strap direction — material, width, thickness — plus quantities and target market. HongDing answers with the development path (3D model, mold plan, sampling) and pricing that covers the belt as one system, hardware included.
Custom Hardware: The 3D Model → Mold → Sample Path
One situation makes separating hardware from the strap factory exactly right: you own a signature buckle design and need it made — intellectual property and a brand asset, tooled regardless of which factory assembles the belts. The development path is standard across the industry, and it runs in stages, each with a defined input and output, so you always know what you are approving.
| Stage | What you bring | What comes out |
|---|---|---|
| 1. Concept and 3D/CAD modeling | Reference buckle, sketch or logo artwork; target strap width and finish direction | A 3D model and render for your approval — geometry checked against the strap before any metal is cut |
| 2. Mold development | Approved 3D model; plating and finish direction | A production mold; tooling cost and timing are project-specific and quoted in writing before work starts |
| 3. First-article samples | The mold plus the finish spec: plating type, color reference, surface treatment | Physical buckle samples — inspected on the actual production strap, not on a desk |
| 4. System approval | First articles mounted on production straps; your function limits | A golden sample of the finished belt; bulk starts only after this approval |
On cost and timing, hold your suppliers to conditional answers, because honest ones are conditional. Tooling cost depends on the geometry, the finish and the quantity program — no credible supplier quotes one number before the 3D model is approved. As a public reference, physical samples usually take 2-3 weeks; mold-dependent first articles are scheduled and confirmed in writing before commitments.
In an OEM or ODM program the same stages apply, with your documents controlling each approval; our design and development route covers the concept-to-specification path, including 3D/CAD buckle development.
Plating and Surface Specifications: Write Them or Chase Them
Plating is where hardware programs drift, and the drift is preventable with a written spec. A plating direction like antique brass is a starting point, not a specification — a specification names the plating type, carries an approved color reference per finish, states the surface treatment (polished, brushed, antiqued), and sets scratch acceptance limits. It also fixes the approval procedure: batches approved against the reference under agreed lighting before assembly, because color drift between lots is a batch problem, not a one-time problem.
The table below is the hardware view of failure modes — where each comes from and what belongs in writing before production. Print it as the skeleton of your acceptance criteria; your spec fills in the numbers with the supplier, per product.
| Mode de défaillance | D'où cela vient | What to agree in writing |
|---|---|---|
| Plating color drift between lots | Plating bath and batch variation | Approved color reference per finish; batch approval before assembly; color checked under agreed lighting |
| Scratches on hardware | Setting fixtures, assembly handling, bare packing | Scratch acceptance limits; protective packaging for buckles — film, sleeve or individual bag |
| Plating wear or corrosion | Thin or uneven plating layer | Plating type and thickness spec; a corrosion check such as salt spray exposure (methods per ASTM B117 or ISO 9227), with hours and pass criteria agreed per program |
| Loose hardware after assembly | Setting force mismatched to strap thickness or material | Setting spec per strap material; pull and engagement checks on samples; limits for bulk |
| Buckle function failure | Prong-to-hole mismatch, spring or ratchet defects | Function test on the assembled belt: prong seats every hole, buckle action and ratchet engagement pass conditions |
| Logo defects on hardware | Stamping or laser setup on curved, plated surfaces | Logo artwork frozen with the golden sample; orientation and legibility limits |
Two compliance points belong next to that table. For corrosion, salt spray methods (ASTM B117, ISO 9227) are the recognized reference — which method, how many hours, and what counts as a pass are program decisions, not defaults. For the EU market, articles in prolonged skin contact fall under nickel-release restrictions in REACH (EC) 1907/2006, Annex XVII — whether your buckle is in scope depends on the article and its use, so confirm it with your supplier and compliance team; for US children’s belts, CPSIA requirements apply.
Blanket claims of certified hardware are a red flag, not a reassurance.
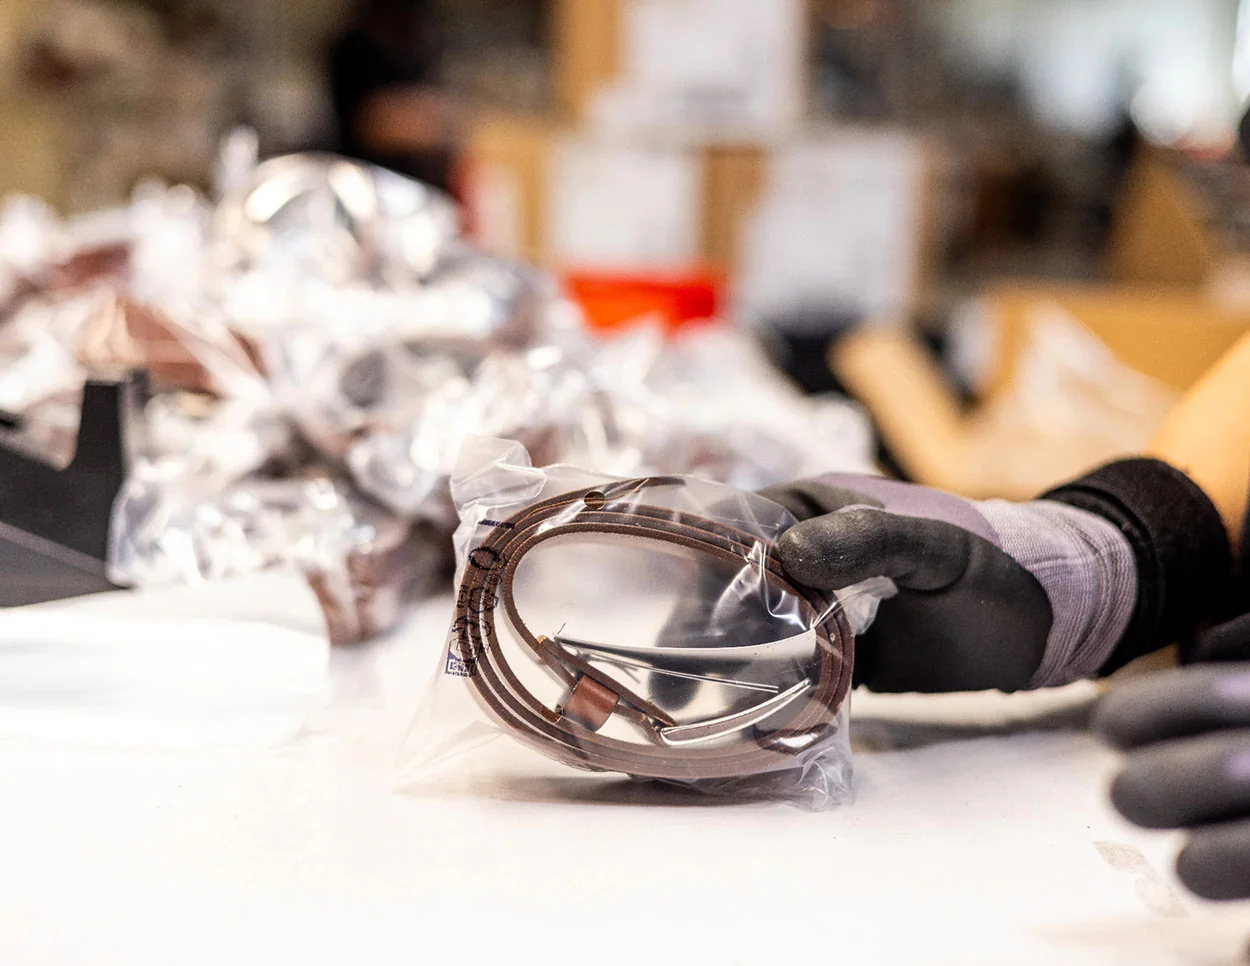
Packaging is the last line of surface defense, and it is a spec, not an afterthought. Buckles wrapped in protective film or sleeved individually survive assembly and transit; hardware packed bare against straps and other buckles arrives pre-scratched, and the dispute over whose scratch it is has no clean answer. Our quality control process checks hardware on the assembled belt at the pre-shipment stage — plating, function, labels and packing together, because that is the product your customer receives.
MOQ Logic When You Buy the Parts Separately
Minimum order quantity in belts is program-specific — it depends on material, construction, SKU mix and packaging, and a credible supplier confirms it after the program is defined, not in the first email. The component route multiplies that uncertainty instead of removing it. Hardware minimums commonly apply per finish or per plating color, so a program with three buckle finishes across four styles can trigger several hardware MOQs on top of the strap factory’s minimums, plus an assembly batch — a stack that can quietly exceed the finished-program quantity you actually needed.
Tooling follows the same stacking logic. A custom mold amortized across a large program disappears into the unit cost; the same mold across a small component order makes each buckle expensive before it has even met a strap. Before you split the program, ask each vendor two questions: what exactly is the minimum per finish and per part, and who holds the excess inventory when the quantities do not align.
If the answers require you to hold stock of parts you cannot use alone, price that inventory into the comparison — a real cost of the component route that never appears on a quote.
Assemble In-House or Buy Finished Belts?
The last version of the parts-or-system question is assembly itself. The factors are concrete:
- Contrôle de la quincaillerie — a specific, licensed or signature buckle may require component sourcing plus your own assembly.
- Capability — assembly means setting equipment, setters who can hold torque and pull limits, and a bench that can catch the interface failures listed earlier. Without that bench, you are the test bench.
- Inventory shape — parts inventory is flexible (one buckle across many straps) but demands warehousing and working capital; finished-goods inventory is simpler but committed per SKU.
- Warranty boundary — assemble in-house and every field failure, whatever its origin, is your failure to diagnose. Buy finished and the factory owns the whole product.
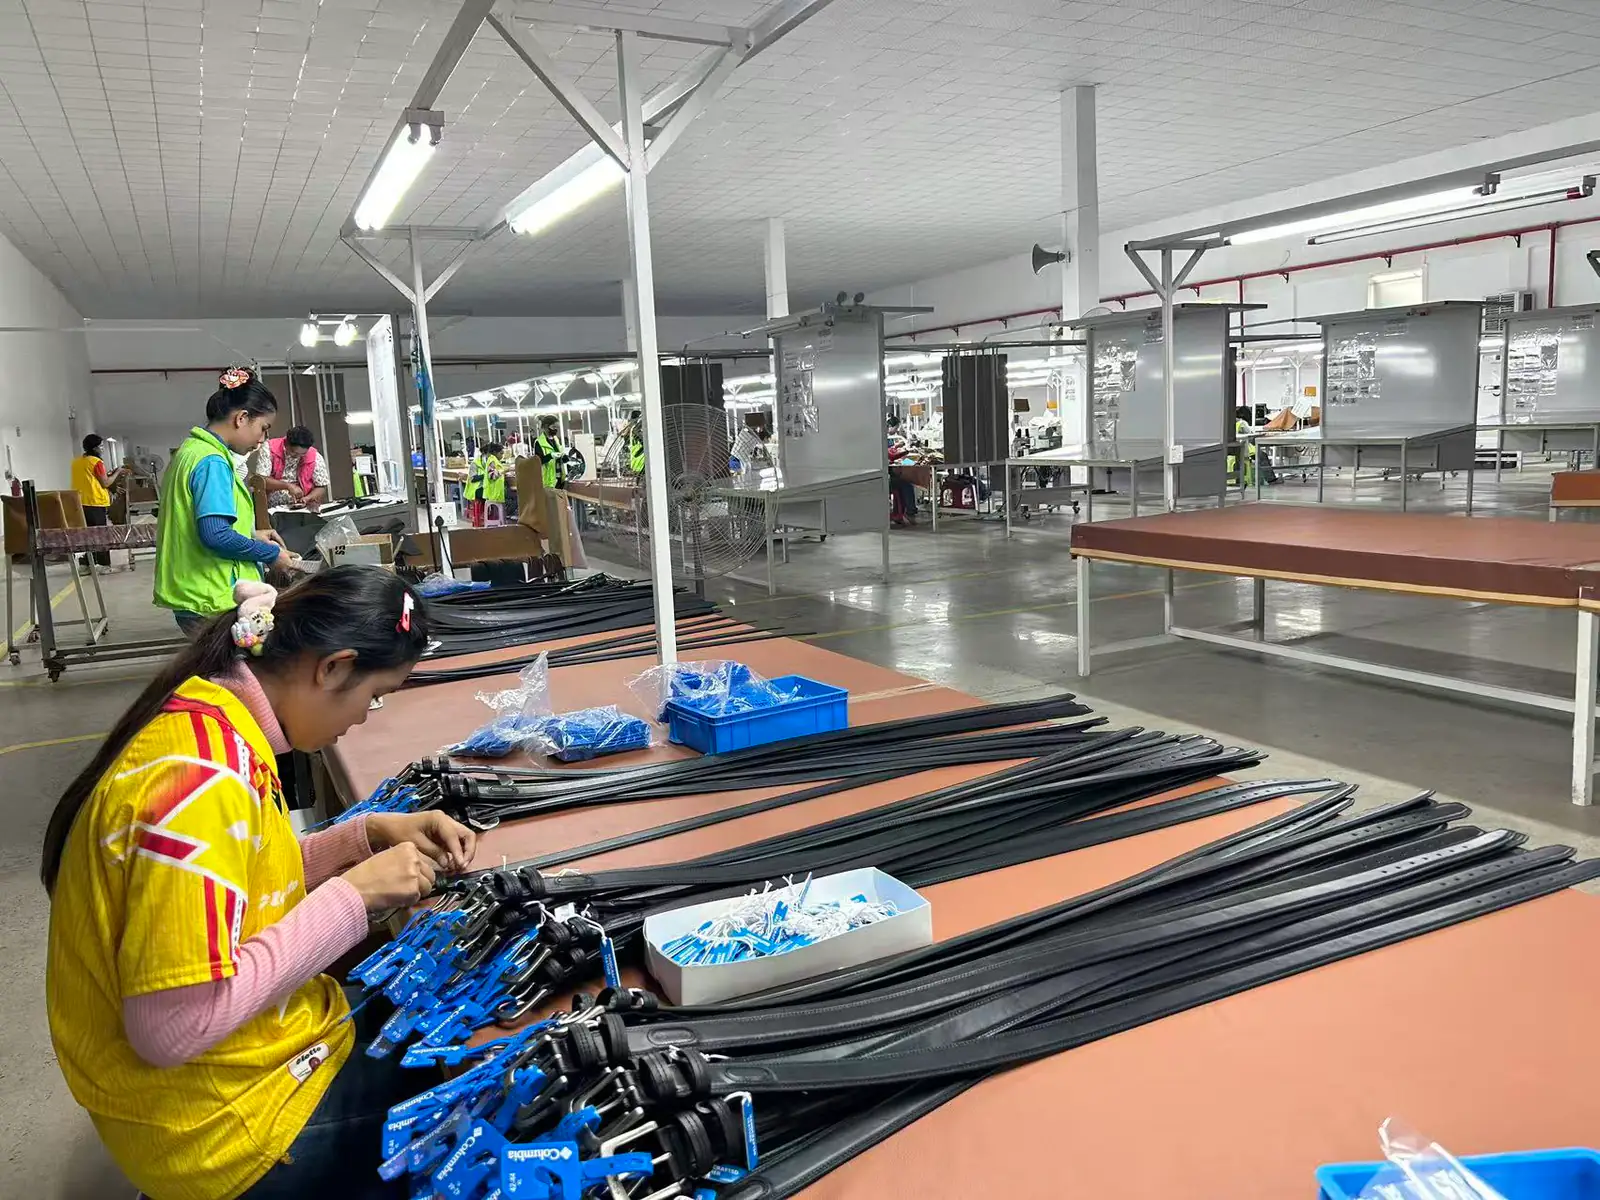
For retail programs — belt walls, seasonal lines, private label launches — the finished route wins on almost every factor: the SKU is the assembled belt, and reorders live or die on the golden sample repeating. The component route earns its place for brands whose hardware is the product. Either way, the approval workflow is the same discipline: prototype, golden sample, written limits, bulk only after the system approval — our sampling process lays out the stages.
Supplier qualification and product release remain separate from buckle-and-strap sourcing. Check site-specific ethical-trade evidence with the SMETA audit guide, then define finished-belt workmanship decisions in the AQL inspection guide.
Questions fréquentes
Can I buy belts and buckles wholesale from one supplier?
Yes — with one condition to understand first: belt factories do not cast their own metal. Even a factory that develops buckles in-house, as we do with 3D/CAD development, has molds cut and parts plated by hardware industry partners. One-supplier sourcing means the factory selects, specifies and owns the hardware inside your belt program — the metal still comes from the hardware world, but the interface risk sits with one accountable party instead of with you.
Is it cheaper to source buckles separately from the straps?
Sometimes on the part price — a hardware vendor casting thousands of one buckle can beat a belt factory on the component alone. The full cost is different: two or three minimums stack instead of one, assembly and its inspection move to your side, and any incompatibility between buckle and strap becomes your diagnosis project. Separation pays when you already control hardware designs and hold assembly capability; otherwise the apparent saving is usually spent on coordination.
How does custom belt buckle development work?
The standard path runs in four stages: 3D/CAD modeling from your reference or artwork, mold development, first-article samples, and approval of the buckle mounted on the production strap. Tooling cost and timing are project-specific — they depend on the geometry, the finish and the quantity program, and they belong in a written quotation before any metal is cut. Bulk production starts only after the system approval, never after a desk inspection of the buckle alone.
What belongs in a buckle plating specification?
At minimum: the plating type, an approved color reference per finish, the surface treatment (polished, brushed, antiqued), scratch acceptance limits, and a corrosion check such as salt spray exposure per ASTM B117 or ISO 9227, with hours and pass criteria agreed per program. For the EU, confirm whether nickel-release restrictions under REACH (EC) 1907/2006 Annex XVII apply to your article; for US children’s belts, CPSIA requirements apply. Every point is written, not implied.
Do belt MOQs include the buckles?
In an integrated program, the quoted minimum covers the finished belt — strap, hardware, assembly and packaging as one product. The number depends on material, construction, SKU mix and packaging, so a credible supplier confirms MOQ after the program is defined. When you source parts separately, hardware minimums — often applied per finish or per plating color — stack on top of the strap minimums and on top of any assembly batch.
Why We Write This
HongDing is a custom belt development and manufacturing partner for brands, retailers, wholesalers and sourcing teams. Buckle development — 3D/CAD modeling through molds and first articles — sits inside our development scope, so we are, openly, the integrated side of the argument in this guide. We write it anyway because the component route is legitimate for buyers who control their hardware and hold assembly capability, and because the failure pattern in the scenario above is entirely avoidable with one rule: approve hardware on the strap it ships on, and only on that strap.
References and Sources
- HongDing development scope including 3D/CAD buckle development, materials and hardware sourcing — hdbelt.com/design-development, hdbelt.com/oem-odm
- Belt sampling and approval workflow — hdbelt.com/sampling; quality control process — hdbelt.com/quality-control
- EU REACH Regulation (EC) No 1907/2006 (incl. Annex XVII nickel-release restrictions) — EUR-Lex
- US Consumer Product Safety Improvement Act (CPSIA) — CPSC
- ASTM B117 and ISO 9227 (recognized salt spray corrosion test methods), cited as test-method references
- Company facts stated on this page follow the HongDing company knowledge base, version 1.0, 2026-09-01
Deciding between parts and systems for your next belt program? Send us your RFQ — bring the buckle reference or logo artwork, the strap direction, quantities and target market, and the answer comes back as a development path and pricing that treats the belt as one product, hardware included.