By Kevin · Updated September 5, 2026
L'inspection AQL est une méthode statistique d'échantillonnage d'acceptation, et non une garantie que chaque courroie est exempte de défauts. Elle aide un acheteur à décider d'accepter ou de rejeter un lot défini à l'aide d'un échantillon aléatoire et de règles de défauts convenues. Le plus difficile arrive avant que l'inspecteur n'ouvre un carton : définir le lot, le niveau d'inspection, les classes de défauts, les limites critiques et la norme de référence.
- L'AQL est un outil de disposition de lot ; il ne remplace pas le contrôle des processus ni les contrôles 100% pour les risques critiques.
- Précisez par écrit l'édition de la norme, la définition du lot, le niveau d'inspection, le plan d'échantillonnage et les seuils de défauts.
- Constituez une bibliothèque de défauts spécifique aux courroies avec des photos et des tolérances mesurables.
- Séparez l'échantillonnage de la qualité d'exécution des tests fonctionnels, des tests réglementaires et de la vérification des quantités.
Ce que signifie AQL — et ce qu’il ne signifie pas
La limite de qualité d’acceptation est utilisée dans un plan d’échantillonnage statistique. Le plan convertit la taille du lot et le niveau d’inspection en un code de taille d’échantillon, puis associe l’AQL sélectionné aux nombres d’acceptation et de rejet. L’inspecteur compte les unités non conformes ou les défauts selon la méthode convenue ; le résultat étaye une décision de disposition pour le lot.
L’AQL est souvent mal interprété comme “ l’usine peut expédier ce pourcentage de pièces défectueuses ”. Ce n’est pas une interprétation sûre. Un lot échantillonné peut contenir des défauts que l’échantillon ne révèle pas. La méthode maîtrise le risque de décision selon des paramètres définis ; elle ne certifie pas chaque unité. La maîtrise des processus, les échantillons approuvés, les contrôles des matières entrantes et les inspections en ligne restent nécessaires.
Contexte des normes : ASQ — normes d’échantillonnage Z1.4 et Z1.9 et ISO 28590:2017.
Cinq entrées doivent être fixées avant l’échantillonnage
Les litiges commencent souvent parce que l’acheteur donne un numéro d’AQL mais omet le niveau d’inspection ou l’édition de la norme. L’usine choisit alors une taille d’échantillon qui l’arrange, tandis que l’inspecteur suppose une autre règle. Fixez les entrées suivantes avant la date d’inspection et consignez-les dans le bon de commande ou la réservation d’inspection.
| Entrée | Décision à consigner | Pourquoi c’est important |
|---|---|---|
| Lot | UGS, couleur, gamme de tailles, quantité et statut d’achèvement | Un échantillon ne peut pas représenter des marchandises en dehors de la population définie. |
| Norme | Édition nommée de l’ANSI/ASQ Z1.4, de la série ISO 2859 ou méthode du client | Les lettres de code et les règles de décision doivent provenir d’une seule source contrôlée. |
| Niveau d'inspection | Niveau général ou spécial indiqué par l’acheteur | Cela influence la taille de l’échantillon et l’effort d’inspection. |
| Plan | Simple/double/multiple ; normal/renforcé/réduit lorsque autorisé | Empêche la règle de changer après la consultation des résultats. |
| Seuils de défauts | Critères critiques, majeurs et mineurs et NQA | Relie les observations aux nombres d’acceptation. |
L’ANSI/ASQ Z1.4 décrit l’échantillonnage par attributs et inclut les systèmes d’inspection normal, renforcé et réduit. Le passage entre ces états suit des règles de commutation ; il ne doit pas être utilisé à la légère pour augmenter ou réduire la taille de l’échantillon pour une commande unique. Si votre client impose un autre plan, cette exigence prévaut.

Choisissez le niveau d'inspection en fonction du risque et de la charge de test.
Les niveaux d'inspection généraux sont couramment utilisés pour la qualité de fabrication globale, car l'inspecteur peut examiner de nombreux attributs sur chaque ceinture sélectionnée. Les niveaux spéciaux fournissent des échantillons plus petits pour les contrôles coûteux, destructifs ou chronophages. Un niveau spécial n'est pas un raccourci pour l'inspection visuelle ordinaire ; il modifie la protection assurée par le plan.
Inscrivez le choix à côté de chaque contrôle. L'aspect général et les dimensions peuvent utiliser le niveau général de l'acheteur, tandis qu'un test destructif de couture ou de composant peut utiliser un niveau spécial approuvé séparément ou un échantillon fixe. Les essais réglementaires en laboratoire se situent en dehors de ce plan d'échantillonnage visuel. L'acheteur—et non le fournisseur le jour de l'inspection—doit approuver chaque voie d'échantillonnage réduite.
Classez les défauts des ceintures avant que l'inspecteur ne les voie.
AQL tables cannot decide whether a crooked logo is major or minor. That is a commercial and risk decision made by the buyer. Create a defect library with photographs, locations, measurable limits and classification. Review it with the factory and inspection company before mass production.
| Class | Working definition | Belt examples to consider | Decision note |
|---|---|---|---|
| Critical | Could create an unsafe or legally nonconforming product | Prohibited sharp point, restricted-substance failure, wrong mandatory warning | Often zero-acceptance or separately controlled; buyer defines rule |
| Major | Likely to cause return, functional failure or material deviation | Buckle will not lock, wrong length tolerance, cracked strap, incorrect logo | Set the agreed AQL and visual boundary |
| Minor | Noticeable departure that does not materially impair use | Small non-prominent stitch or finish variation within defined limits | Avoid subjective definitions such as “not perfect” |
Use product-specific examples. On a reversible belt, failure of the swivel mechanism is functional. On a dress belt sold for uniform use, a shade mismatch across the delivered set may be commercially major. Natural grain variation can be acceptable or unacceptable depending on the sealed standard. Translate these expectations into observable rules.
A Belt Inspection Checklist That Matches the Specification
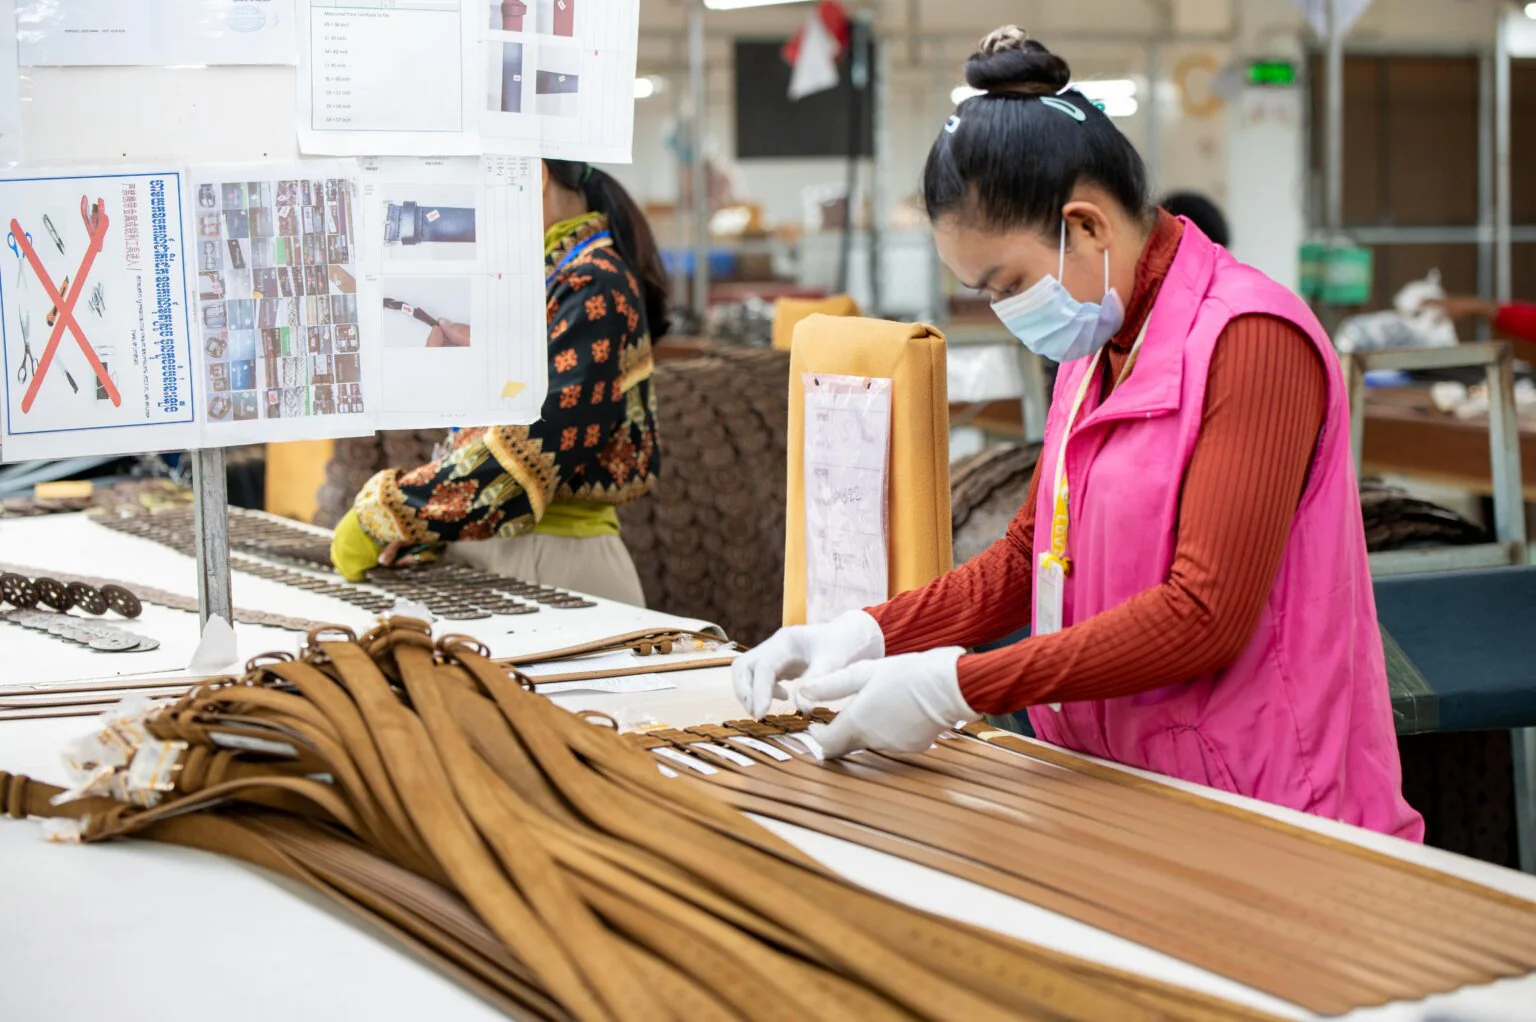
Inspection should trace to controlled references. The approved sample shows the intended overall result, while the drawing and tolerance table govern measurements. The BOM identifies materials, and approved artwork governs logos and packaging. When sources conflict, the inspection plan should state the order of precedence.
| Inspection area | Examples | Référence |
|---|---|---|
| Identity and quantity | SKU, colour, size, assortment, carton count | PO and packing list |
| Dimensions | Overall length, width, hole spacing, tip and buckle dimensions | Drawing and tolerance table |
| Matériaux | Face, lining, reinforcement, buckle finish and approved shade | BOM and sealed sample |
| Workmanship | Stitching, edge, holes, rivets, logo and surface | Defect library |
| Fonction | Buckle engagement, keeper fit, reversible/ratchet action | Test instruction |
| Emballage | Barcode, label, warning, polybag and carton marks | Approved artwork and pack spec |
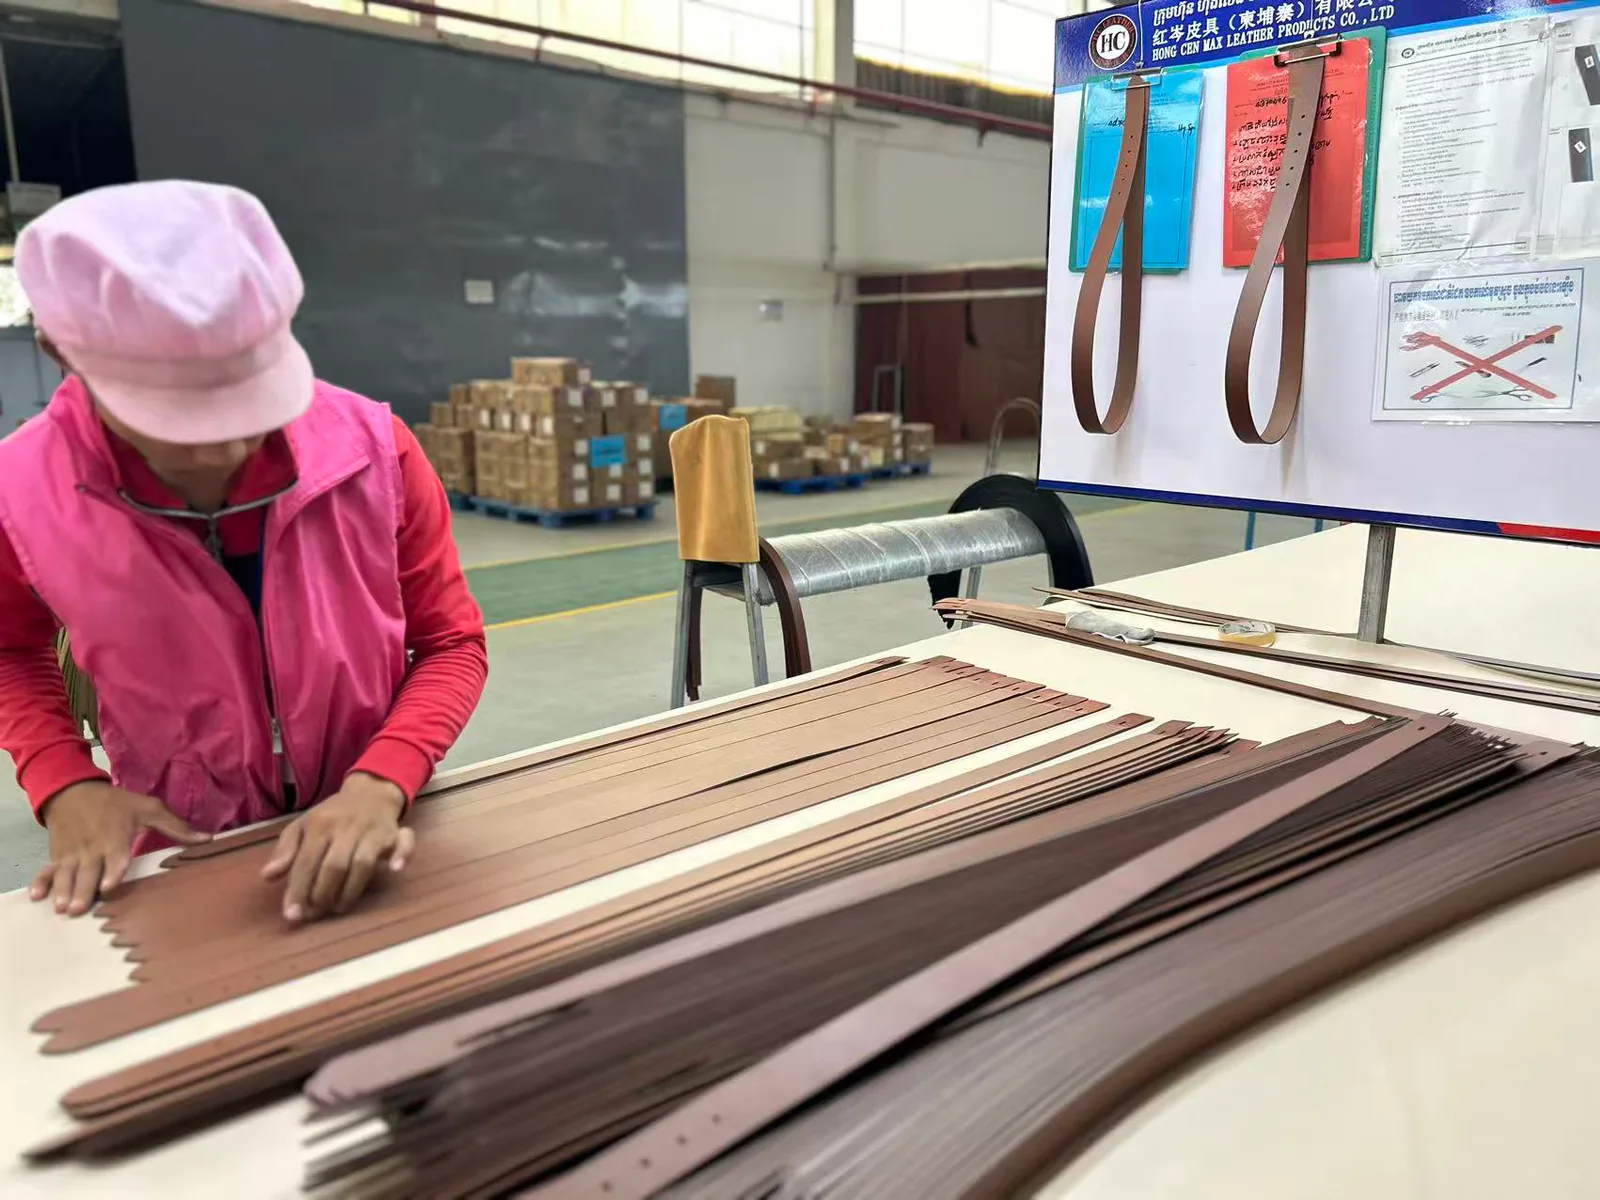
Randomization is equally important. The inspector should select cartons across accessible locations and draw units without supplier preselection. Record which cartons and units were sampled. If the lot is incomplete or inaccessible, report the limitation instead of presenting the result as representative of a finished lot.

Make the Acceptance Decision Without Moving the Goalposts
How to read the sampling tables
- Find the declared lot-size band in the first table of the named standard.
- Move across to the buyer-approved inspection level to obtain the sample-size code letter.
- Open the correct sampling-plan table: single, double or multiple; normal, tightened or reduced as authorized.
- Use the code-letter row to identify the sample size.
- For each defect class, move to the chosen AQL column and record its acceptance and rejection numbers.
- Inspect the randomized sample, count under the agreed unit-of-counting rule and decide each class separately.
This walkthrough deliberately omits a numeric Ac/Re example. The numbers must come from the controlled edition your contract names, and a copied online chart may use another plan or omit switching rules. Put a controlled table reference in the inspection booking so the buyer, factory and inspector use the same row and column.
Count each observed defect under the agreed class and apply the table’s acceptance/rejection number. Define whether several defects on one unit count as separate defects or one nonconforming unit under your method. Record the result by class; a combined defect total can hide a critical problem.
If the lot fails, quarantine it. Review evidence, agree containment, root-cause analysis, rework or 100% sorting, and a reinspection rule. Do not simply remove the failed sample and draw another. Any conditional release should identify the accepted deviation, affected quantity, approver and customer impact.
What AQL Sampling Cannot Prove
A workmanship sample does not replace chemical compliance testing, performance testing or legal review. Restricted substances generally require a risk-based laboratory plan. Buckle strength, corrosion, flex endurance or adhesion may require dedicated methods and sample quantities. A barcode scan on sampled packs does not prove every unit carries the correct label.
Critical risks may justify prevention controls, verified material certificates, process checks or 100% screening. AQL should be one layer in the control plan, not the only release mechanism. The broader Cadre de contrôle qualité HongDing shows how material, production and final checks can connect.
Align Buyer, Factory and Inspector Before Production
Hold a pre-production quality review for new styles or high-risk changes. Confirm the sealed sample, tolerances, defect library, test methods, pack configuration, lot readiness definition and decision owner. Send the same controlled files to the factory and third-party inspection company. Version numbers prevent an outdated drawing from becoming the inspection standard.
HongDing’s custom program process moves from specification and sampling into bulk production and release. Buyers receive more reliable evidence when quality criteria are defined during development, not invented during final inspection. The OEM belt guide provides the commercial context for locking specifications and approvals.

Need a belt-specific inspection plan?
Send the style drawing, order quantity, target market and customer standard. We can align factory records and inspection checkpoints around your approved specification.
AQL Inspection-Plan Template
The following fields make an inspection instruction auditable. Replace the example with your own risk decisions; do not copy a generic AQL value simply because it appears in another brand’s manual.
| Plan field | Example of a controlled entry |
|---|---|
| Lot definition | Style ABC, black, sizes 80–110 cm, 4,800 finished units available together |
| Sampling basis | ANSI/ASQ Z1.4, stated edition; single sampling, normal inspection; General Level II |
| Defect rules | Critical/major/minor definitions in attached defect library; selected AQLs stated by buyer |
| Functional tests | Buckle operation and dimensional checks with separate sample or frequency |
| Preuves | Random-carton record, sample list, defect photos, counts and measurement sheet |
| Décision | Buyer accept, conditional release, sort/rework or reject; named approver |
Do not pool different SKUs by convenience
A purchase order containing several styles, colours and sizes needs an explicit lot rule. Pool only items that the buyer has decided form one sufficiently uniform population under the plan. Different strap materials, buckle mechanisms, factories, production dates or high-risk colourways may need separate lots. If sizes share the same construction, the buyer can still require proportional or minimum coverage by size.
The inspector should record how the sample is allocated across SKUs, colours and sizes before opening units. Allocation must not allow the supplier to present only the easiest cartons. When a small high-risk SKU would disappear inside a pooled sample, specify a minimum draw or inspect it separately.
PO inspection clause fields
A complete clause names the standard and revision; lot and SKU grouping rules; inspection level and sampling plan; critical, major and minor definitions; defect library and approved references; when goods must be complete and accessible; who books and pays for the first inspection; who bears reinspection and sorting costs after a supplier-caused failure; whether payment or shipment is held pending release; who has release authority; and how deviations are approved.
Structural example: “Final inspection will follow [named standard and revision], [plan and level], using the attached defect library and approved sample. Lots are defined by [factory/style/material/date rule]. Goods must meet the buyer-defined readiness rule by the booking date. Failure triggers quarantine and the buyer’s written disposition; rework, sorting, reinspection cost and shipment release follow the agreed responsibility clause.” Legal review should adapt the language to the contract.
Add the booking date, inspection location, allowed rework, report distribution and release deadline. After shipment, feed returns and defect trends back into the defect library. This guide does not present a HongDing defect rate or buyer-approved AQL setting; those values are program-specific and must come from the signed inspection plan.
Questions fréquentes
What does AQL mean in product inspection?
AQL is the quality level used with an acceptance-sampling plan to determine sample size and acceptance or rejection numbers for a lot. It is not the percentage of defects a supplier is allowed to ship in every order.
Which AQL level should I use for belts?
There is no universal belt setting. The buyer should select inspection level and class-specific AQL values according to risk, customer requirements, history and the referenced standard. Critical defects are often handled more strictly or checked separately.
Does AQL inspection check every belt?
No. It evaluates a randomly selected sample from a defined lot. Quantity checks, critical safety controls or high-risk functions may require separate or 100% inspection.
Can I change the sample after defects are found?
Do not expand or redraw the sample informally to chase a desired result. Follow the declared plan and escalation procedure, or document a new inspection with a clear reason.
What happens after an AQL failure?
Quarantine the lot, review defect evidence and root cause, agree rework or sorting, and reinspect under a documented rule. Shipment release should be a buyer decision, not an automatic result of supplier rework.
How is the AQL sample size selected?
The buyer defines the lot and inspection level under a named standard edition. The lot-size row and inspection-level column produce a code letter; the selected plan table converts that code into sample size and class-specific acceptance/rejection numbers.
What is a critical defect on a belt?
A critical defect is one the buyer defines as creating an unsafe or legally nonconforming product, such as a prohibited sharp point or wrong mandatory warning. The classification and acceptance rule must be agreed before inspection; AQL does not create a universal list.